UniCare is a premier professional supplier and industrial pioneer of natural active ingredients, specialty botanical extracts, and advanced functional nutrition powders, including high-potency Vitamin C juice powders. Our ingredients are widely utilized across dynamic international sectors such as dietary supplements, functional foods, clean-label cosmetics, and rigorous pharmaceutical applications.
We focus relentlessly on product development, molecular stability, and complete batch-to-batch traceability. By forging deep, strategic alliances with elite Chinese manufacturing facilities operating under comprehensive quality management certifications—including GMP, EU-GMP, CEP, ISO9001, ISO22000, and HACCP—we guarantee that our global partners receive standardized, safe, and ultra-pure raw materials.
Unlocking novel biochemical properties in functional herbs and natural fruit powders for next-generation wellness products.
Pushing the boundaries of extraction science, drying technologies, and enzymatic modification processes.
Utilizing state-of-the-art automated control systems to guarantee maximum active compound preservation.
Fostering an empowering workplace environment and contributing sustainably to agricultural communities worldwide.
UniCare attaches paramount importance to hardware infrastructure, maintaining partnership ownership of one of the largest and most technologically advanced extraction and spray-drying facilities in China. Our automated production ecosystem ensures uniform particle distribution, excellent solubility, and exceptional thermal stability for delicate components like Vitamin C in natural juice powders.
The entire production line operates under an advanced, intelligent, automatic control architecture. To date, our partnered manufacturing infrastructure features two dedicated GMP standard workshops housing six multi-functional extraction lines, alongside specialized fermentation facilities capable of processing over 30,000 metric tons of raw botanical and fruit materials annually.

Strict compliance across all cleanroom processing and packaging operations.

Internationally validated quality benchmarks for global pharmaceutical exports.

Automated control loops maintaining precise thermal and pressure profiles.

Equipped with industry-leading multi-stage countercurrent extraction systems.

Massive economies of scale ensuring stable, continuous international supply.

Three annular dynamic countercurrent and two multi-functional extraction lines.
The global demand for clean-label, plant-derived functional ingredients has surged exponentially over the past decade. Among these, wholesale Vitamin C juice powders—derived from potent natural fruit sources such as Acerola Cherry, Camu Camu, Rosehip, and Seabuckthorn—have become cornerstones of the functional beverage and dietary supplement industries. Unlike synthetic ascorbic acid, natural Vitamin C juice powders provide complex bioflavonoids, co-enzymes, and synergistic phytonutrients that significantly enhance human bioavailability and antioxidant efficacy.
As a leading factory and global supplier, UniCare bridges the gap between large-scale agricultural cultivation and international brand manufacturing, delivering fully standardized, high-solubility Vitamin C fruit powders that satisfy the stringent regulatory frameworks of the US FDA, European Food Safety Authority (EFSA), and global pharmacopeias.
Preserving the integrity of Vitamin C during industrial extraction and spray-drying is a formidable thermodynamic challenge. Ascorbic acid is highly sensitive to heat, oxidation, and pH fluctuations. UniCare solves this challenge through proprietary low-temperature vacuum concentration and advanced microencapsulation spray-drying technologies.
| Parameter | Specification Standard | Testing Method |
|---|---|---|
| Active Vitamin C Content | 17% – 25% (Natural Fruit Standardized) | HPLC / Titration |
| Appearance | Fine Pale Yellow to Orange-Yellow Powder | Organoleptic / Visual |
| Solubility | Instant Dispersibility in Cold Water | Visual Inspection (1g in 50ml H2O) |
| Heavy Metals (Lead, Arsenic, Cadmium, Mercury) | < 1.0 ppm max per element | ICP-MS |
| Microbial Limits | Total Plate Count < 1000 CFU/g, Yeast & Mold < 100 CFU/g | Pharmacopeial Enumeration |
Global procurement directors across North America, Europe, and Asia-Pacific require more than just raw material supply; they demand robust supply chain resilience, regulatory compliance, and localized application support. UniCare's Vitamin C juice powders are engineered for seamless integration across diverse product categories:
United New Life and its manufacturing partners have established an industry-leading quality assurance architecture. Every batch of Vitamin C juice powders and botanical extracts undergoes rigorous multi-stage screening in our CNAS-qualified central laboratories.
| Testing Category | Specific Parameters Analyzed |
|---|---|
| Active Ingredient Analysis | Assay quantification, structural identification, bioflavonoid ratio verification. |
| Hazardous Substance Analysis | Heavy metal screening (ICP-MS), organochlorine pesticide residues (GC-MS-MS), residual solvents (GC). |
| Microbiological Profiling | Total viable count, Escherichia coli, Salmonella, yeast, mold, and pathogen detection. |
| Raw Material Traceability | Pesticide screening, non-GMO verification, botanical origin authentication. |
| Regulatory & Stability Testing | Real-time and accelerated shelf-life stability studies compliant with ICH guidelines. |
2x Agilent 1290 UHPLC, 4x Agilent 1260 HPLC, 2x Shimadzu LC-20AT systems for high-resolution chromatographic assay.
Shimadzu GC-2010 gas chromatograph and evaporative light scattering detectors (ELSD 2000ES) for specialized purity testing.
Shimadzu AA-7000 atomic absorption system ensuring parts-per-billion sensitivity for heavy metal contaminants.
UniCare reinvests 10% of its annual net profit directly into research and development. Beyond refining conventional botanical extraction, we operate an advanced R&D department dedicated to natural fermentation products. Through deep academic collaboration with institutions like the Beijing University of Chemical Technology, we pioneer breakthrough enzymatic processes that disrupt traditional manufacturing and elevate bio-active yields.
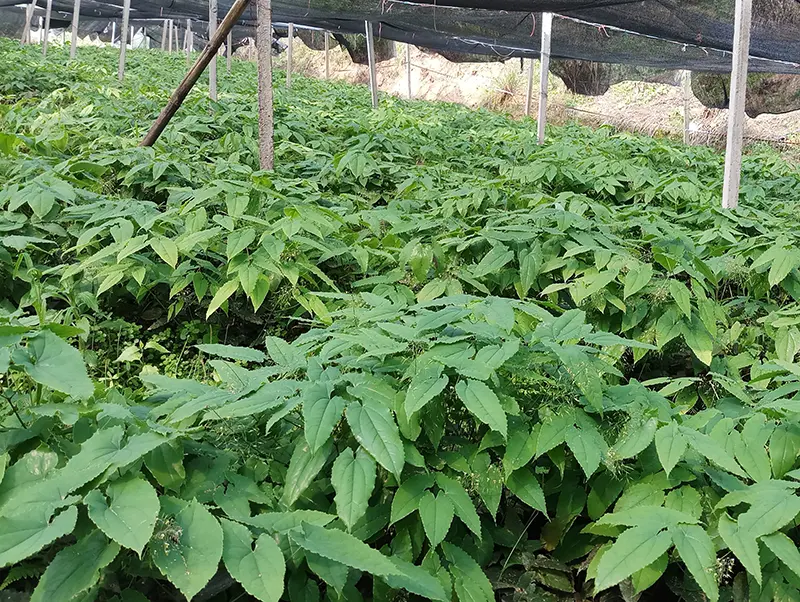
Superior extracts originate from immaculate agricultural management. We have established proprietary GACP-compliant planting bases for high-demand botanicals and fruit sources. By collaborating with agricultural research partners on high-content seedling hybridization and genetic optimization, we control quality at the root level while continuously reducing production costs to benefit our global clientele.