Discover our primary export formulations engineered for advanced industrial applications, strict regulatory compliance, and maximum therapeutic efficacy.
High-purity ellagic acid standardized for nutraceutical formulations.
EU-GMP and CEP certified flavonoid glycosides for cognitive health.
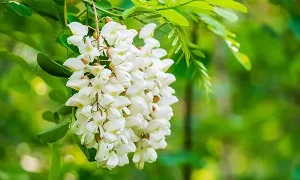
Superior bioavailability bioflavonoid for anti-inflammatory supplements.
As the global health and wellness ecosystem pivots toward preventative healthcare and clean-label functional foods, Blueberry Powder Supplier & Exporters serving New Amsterdam play a pivotal role in bridging high-efficiency manufacturing hubs with dynamic regional consumption centers. New Amsterdam, characterized by its unique demographic profile, burgeoning health-conscious consumer base, and expanding retail infrastructure, represents a high-growth market for antioxidant-rich botanical ingredients. Importers, functional beverage brands, and dietary supplement formulators in New Amsterdam require consistent, high-potency, and analytically verified raw materials that comply with international safety benchmarks.
On a macro-economical scale, the global industrial landscape for premium fruit powders and anthocyanin-rich extracts is projected to witness explosive compound annual growth rates (CAGR). Consumers globally are replacing synthetic additives with bioactive plant components. Blueberry powder, renowned for its dense concentration of anthocyanins, pterostilbene, and dietary fiber, is heavily integrated into sports nutrition powders, infant nutrition, functional smoothies, and clinical dietary supplements. By establishing a streamlined supply chain directly into New Amsterdam, we empower local enterprises to scale their product offerings without compromising on quality or traceability.
What sets our supply network apart is the integration of world-class manufacturing infrastructure based in China, engineered to deliver unmatched economies of scale and strict quality assurance. Our manufacturing partners operate the largest and most advanced extraction facilities in the region, featuring intelligent, fully automated control systems. These facilities house two dedicated GMP workshops equipped with six multi-functional extraction lines, three annular dynamic countercurrent extraction lines, and specialized processing units capable of handling complex botanical matrices.
Furthermore, our production framework includes specialized fermentation lines and multi-ton fermentation tanks dedicated to enzyme-modified bioactives. This technological superiority allows us to optimize extraction yields, reduce unit production costs, and pass those financial efficiencies directly to our B2B partners serving New Amsterdam. Every batch undergoes rigorous standardization to ensure high active ingredient concentration, uniform particle size, excellent solubility, and exceptional microbiological safety.
Committed to scientific excellence, sustainable sourcing, and long-term collaborative growth with global partners.
UniCare is a professional supplier of natural active ingredients. Our products are widely used in various fields such as dietary supplement, food, cosmetics and pharmaceuticals. We focus on product development and quality stability, and insist on growing together with our customers around the world.
UniCare has deep cooperation with several excellent Chinese manufacturers who have complete quality management system certifications, including but not limited to GMP, EUGMP, CEP, ISO9001, ISO22000, and HACCP. Each factory has independent testing capabilities and is equipped with advanced and efficient testing equipment to ensure the high quality and long-term stability of each batch of products.
 Send Inquiry Now
Unlocking untapped therapeutic potentials through advanced phytochemical research.
Iterative enhancement of extraction methodologies and green chemistry practices.
Utilizing cutting-edge machinery to guarantee uncompromised product purity.
Fostering a responsible corporate culture that uplifts society and workforce.
Explore the engineering prowess and hardware superiority driving our global export operations.
UniCare attaches great importance to the hardware conditions of production equipment and operates the largest and most advanced extraction facility in China. Controlled entirely by modern, intelligent automated systems, our facilities process up to 30,000 tons of medicinal and plant raw materials annually, ensuring seamless fulfillment for large-scale commercial buyers in New Amsterdam.

Strict adherence to regulatory manufacturing practices across all operational units.

Certified extraction processes meeting stringent international pharmaceutical benchmarks.

State-of-the-art automated control systems eliminating human error and ensuring batch consistency.

Six specialized production lines including dynamic countercurrent extractors and fermentation tanks.
Controlling quality from seed selection to advanced phytochemical extraction.
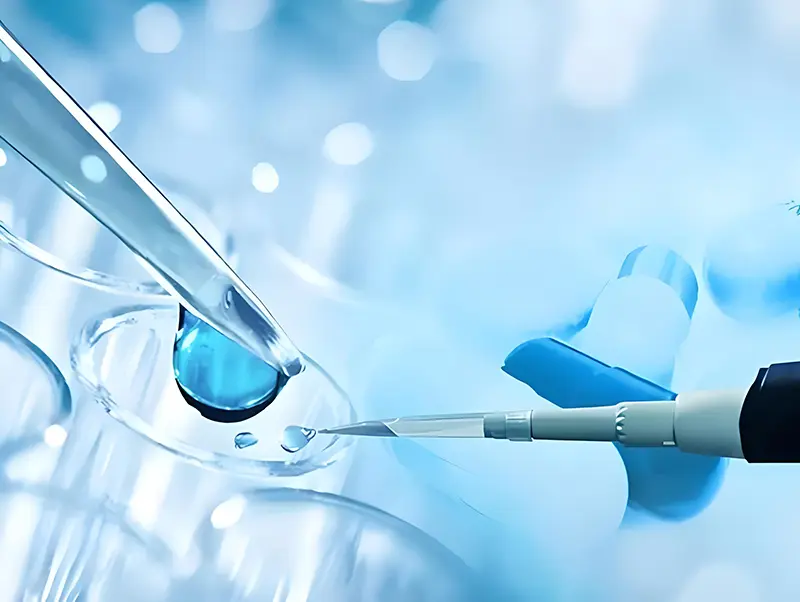
UniCare invests 10% of our annual net profit in research and development. Beyond optimizing existing extraction methods, we maintain a dedicated natural fermentation R&D division. Through our deep strategic collaboration with the Beijing University of Chemical Technology, we pioneer novel pharmaceutical, cosmetic, and health product ingredients, translating cutting-edge science into commercial scale.
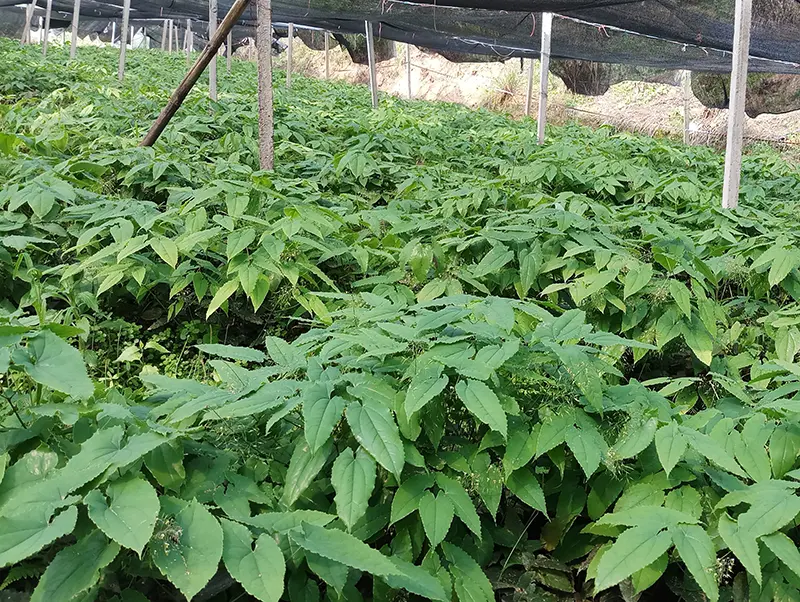
To ensure uncompromising purity, our raw material procurement system extends directly to agricultural land plots, enabling complete batch-level traceability. We partner with specialized farming communities and seedling research firms to cultivate high-yield, high-potency varieties following GACP guidelines, continuously driving down unit costs while maximizing active constituent levels.
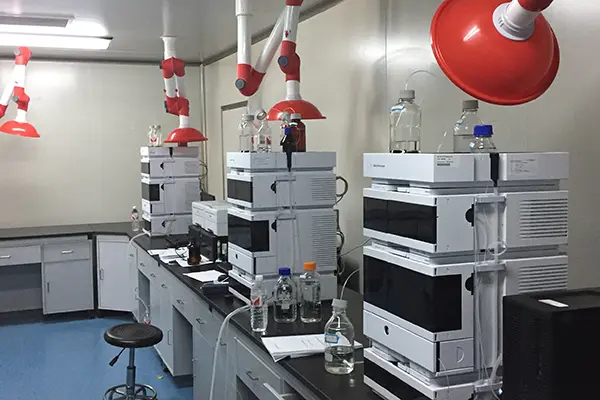
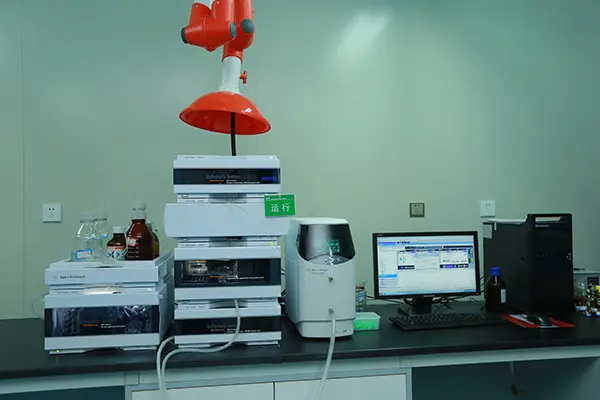
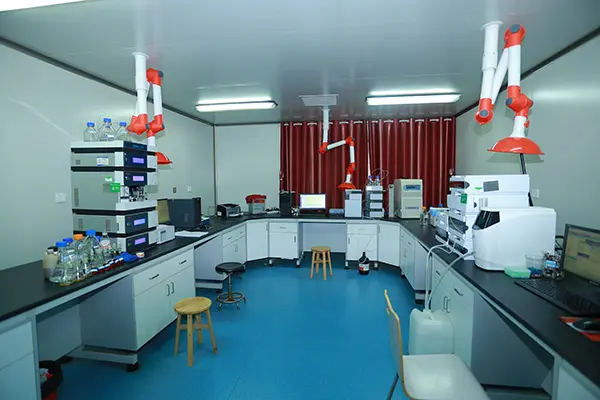
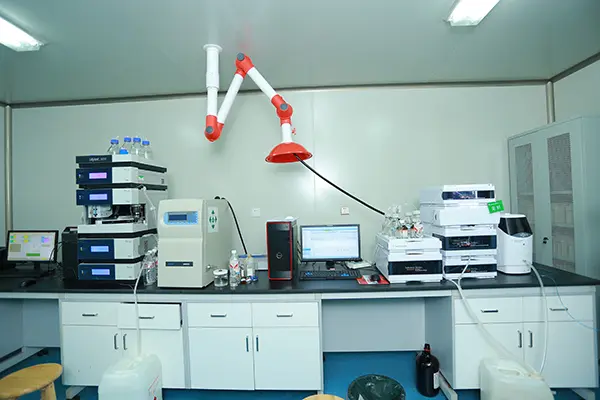
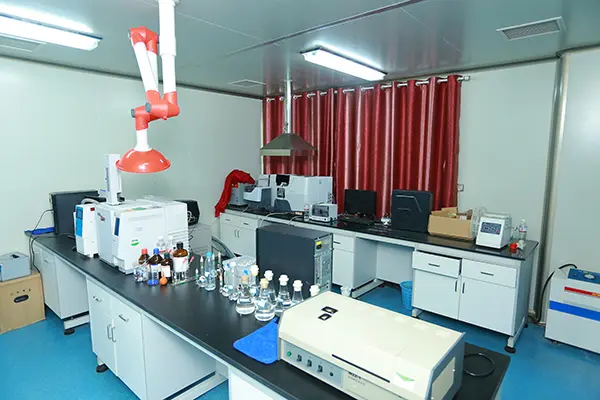
Backed by a CNAS-qualified Central Laboratory and state-of-the-art analytical instrumentation.
United New Life has established a leading and complete quality control system, strictly testing every lot against signature components (HPLC/UV), solvent residues (GC), pesticide residues via GC-MS-MS, heavy metals via ICP-MS, moisture, ash, and microbiological limits.
| Testing Category | Target Parameters |
|---|---|
| Active Ingredient Analysis | Assay, identification, marker compound quantification |
| Hazardous Substance Analysis | Heavy metals (Lead, Arsenic, Mercury, Cadmium, Copper), pesticide residues, solvent residues |
| Microbe Analysis | Total plate count, E. coli, Salmonella, yeast & mold, specific pathogen tests |
| Raw Material Control | Pesticide screening, allergen screening, GMO verification, botanical origin authentication |
| Stability Testing | Real-time and accelerated shelf-life verification studies |
| UHPLC, Agilent 1290 (×2) | HPLC, Agilent 1260 (×4) | HPLC, Shimadzu LC-20AT (×2) |
| ELSD, Shimadzu 2000ES (×2) | Shimadzu GC-2010 (×1) | Shimadzu AA-7000 Atomic Absorption (×1) |
Expert insights addressing common procurement, technical, and regulatory inquiries for New Amsterdam buyers.
Explore our full range of premium certified herbal extracts and active ingredients available for international export.