Discover our elite tier of standardized plant extracts utilized by cutting-edge industrial manufacturers and laboratory researchers globally.
Bridging advanced phytochemical engineering with the strategic industrial needs of Esch-sur-Alzette and international markets.
UniCare is a professional supplier of natural active ingredients. Our products are widely used in various fields such as dietary supplement, food, cosmetics and pharmaceuticals. We focus on product development and quality stability, and insist on growing together with our customers around the world.
UniCare has deep cooperation with several excellent Chinese manufacturers who have complete quality management system certifications, including but not limited to GMP, EUGMP, CEP, ISO9001, ISO22000, and HACCP. Each factory has independent testing capabilities and is equipped with advanced and efficient testing equipment to ensure the high quality and long-term stability of each batch of products.
Send Inquiry Now
Guided by science, driven by sustainable innovation, and dedicated to unmatched purity in every batch.
State-of-the-art infrastructure designed to deliver maximum purity, traceability, and scalable supply for Esch-sur-Alzette enterprises.
UniCare attaches great importance to the hardware conditions of production equipment and has the largest and most advanced extraction factory in China. The entire production line in UniCare is controlled by a modern, intelligent, automatic control system. Until now, UniCare has built up two GMP workshops, containing six multi-functional extraction lines, processing up to 30,000 tons of botanical raw materials annually.
Passed strict China GMP certification standards ensuring pharmaceutical-grade production.
Ginkgo Biloba Extract fully certified meeting stringent European regulatory criteria.
Modern, intelligent, and fully automated extraction control lines for consistent potency.
Annual processing capacity of 30,000 tons of premier medicinal and herbal materials.
Equipped with annular dynamic countercurrent extraction lines and heavy-duty reaction tanks.
Operates China's sole acetone-process extraction line meeting EU GMP specifications.
Six large 20-ton fermentation tanks dedicated to high-efficiency enzyme-modified derivatives.
Rigorous origin control from cultivation plots to final manufactured powder formulation.
Complete analytical validation backed by CNAS-qualified central laboratories and world-class testing instrumentation.
| Testing Category | Parameters Analyzed |
|---|---|
| Active Ingredient Analysis | Assay, structural identification, phytochemical profiling |
| Hazardous Substance Analysis | Heavy metals (Lead, Arsenic, Mercury, Cadmium, Copper), pesticide residues, solvent residues |
| Microbe Analysis | Total aerobic count, Escherichia coli, yeast & mold, specific pathogen testing |
| Raw Material Control | Pesticide residues, allergen screening, GMO testing, botanical origin verification |
| Laws & Regulations Confirmation | Compliance auditing for EU, Chinese, and international market standards |
| Stability Test | Accelerated and long-term shelf-life verification under diverse environmental conditions |
Investing heavily in innovation, genetic optimization, and GACP-compliant agricultural partnerships.
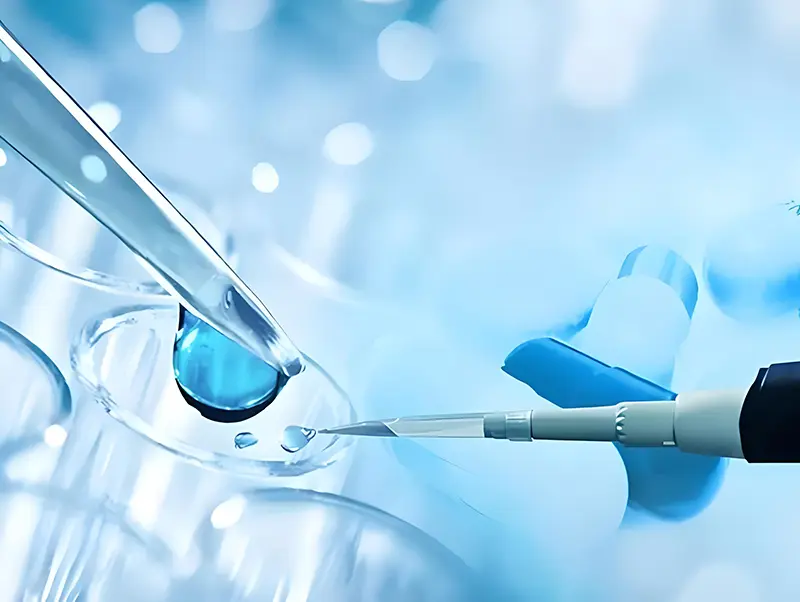
UniCare invests 10% of our annual net profit in research and development. In addition to optimizing traditional natural plant extraction processes, we have established a professional R&D division for natural fermentation products, partnering with institutions like the Beijing University of Chemical Technology to break new ground in pharmaceutical and health supplement applications.
To maintain absolute control over quality, we extend procurement directly to dedicated GACP-certified cultivation bases for Ginkgo, Epimedium, Phellodendron, and Olive Leaf. Through advanced breeding and hybridization programs, we optimize active constituent yields while keeping unit production costs sustainable for our global clients.
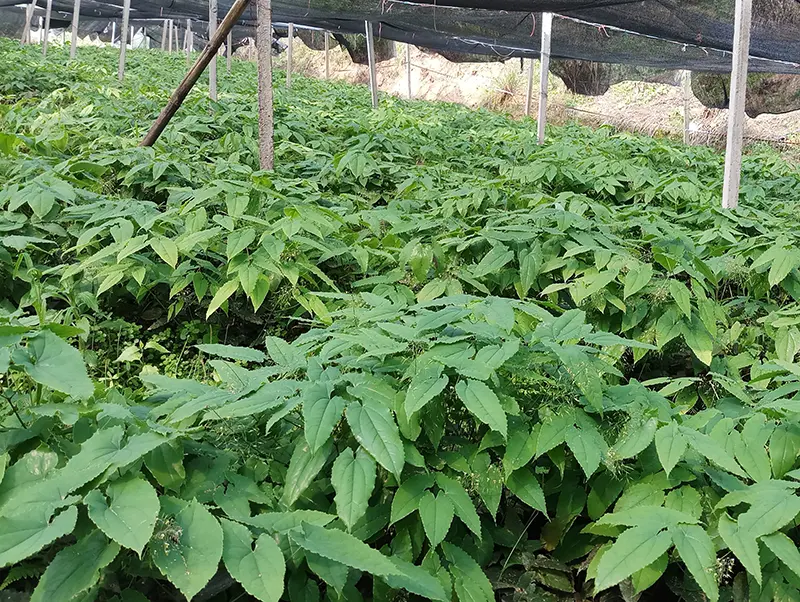
Comprehensive range of extracts tailored for industrial formulation and wholesale procurement.
Navigating regulatory compliance, industrial integration, and future supply chain frameworks in Luxembourg.
Esch-sur-Alzette, as a vital economic engine in Luxembourg, represents a growing hub for advanced biotechnology, health innovation, and specialized food processing distribution. Local enterprises demanding high-grade botanical ingredients, such as premium raspberry powder, require dependable logistics channels, stringent EU food safety adherence, and guaranteed batch-to-batch phytochemical consistency.
International procurement managers face challenges including volatile raw material yields and strict regulatory changes. Our macro-level supply solutions integrate direct farm GACP oversight, intelligent automated extraction, and rigorous HPLC/LC-MS testing. This ensures Esch-sur-Alzette manufacturers receive secure, scalable, and fully compliant raw materials without interruption.
Raspberry powder is extensively used in functional foods, dietary supplements, sports nutrition formulations, and natural cosmetic anti-aging preparations due to its rich antioxidant profile (ellagic acid, anthocyanins, and vitamin C).
All products comply with stringent European Food Safety Authority (EFSA) guidelines, GMP manufacturing standards, and come complete with comprehensive Certificates of Analysis (CoA) verifying heavy metal, pesticide, and microbial safety.
We accommodate both pilot-scale research batches and large commercial volume orders. Please contact our sales team to discuss specific volume requirements.